Measure where the process needs evidence
Product temperatures are measured at defined locations around the heating and holding route. Flow, vessel level, utility condition and pressure are monitored where the selected process and equipment require them. Sensor location, calibration and recording determine what an indicated value means.
A display reading alone is not evidence that every part of a viscous or particulate product completed its required heating history.
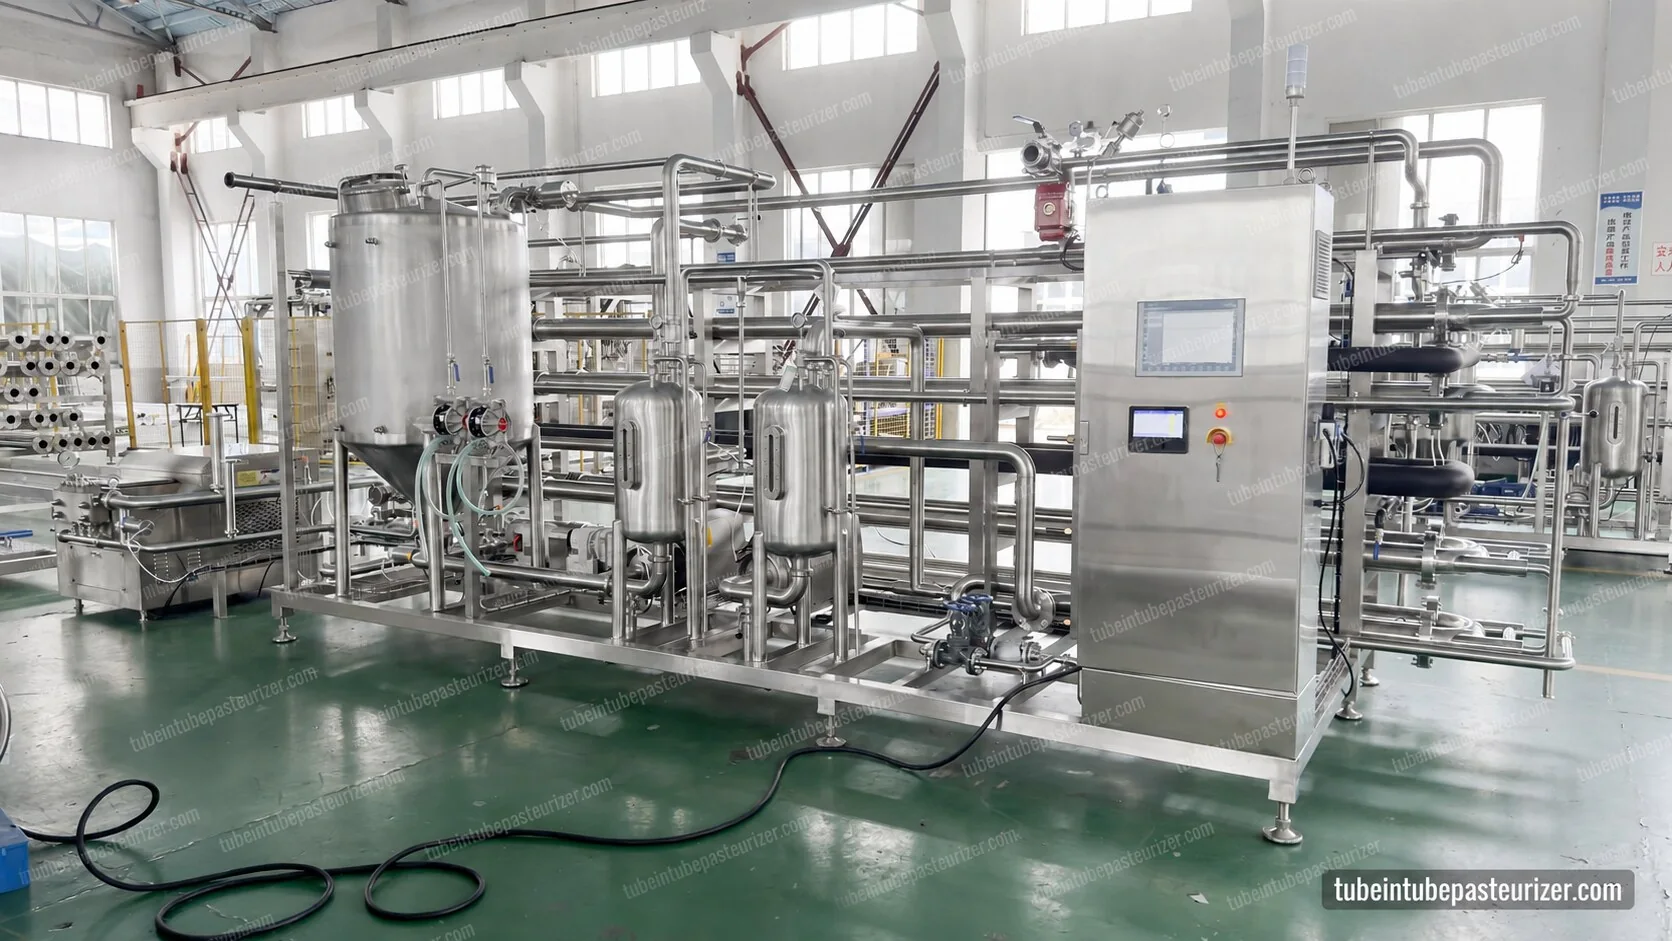
Separate preparation, production and cleaning
Preparation confirms required utilities and circulation before releasing product. Production then maintains selected operating limits. A feed interruption, insufficient heating or downstream stop must lead to the configured safe route and an explicit restart condition.
Cleaning uses the selected CIP path and sequences rather than ordinary product routing. When an SIP step is part of the order, its state and records are specified independently.
Demonstrate the fitted logic
For the actual system, the control review can test instrument readings, alarms, interlocks, route changes and downstream handshake. The supplier and buyer agree which records are delivered at factory and site acceptance.
Product-process and package validation is specific to the food and intended operation. It is not proven by a simulated temperature value or by a generic factory water run.